
Conversion varnish, the catalyzed finish of professional cabinetry, earns its reputation for hardness and chemical resistance only when applied at the correct film thickness. Too thin and the finish never develops its full properties: it stays soft, wears quickly, and fails the chemical resistance it was chosen for. Too thick and it cracks, alligators, or cures with solvent trapped inside, failing differently but just as completely. Film thickness control is therefore not a quality nicety; it is the difference between the finish working and failing, and it is measured, not eyeballed.
Why Thickness Determines Performance
Conversion varnish cures by chemical crosslinking between the resin and the acid catalyst, and that reaction needs a minimum film mass to develop properly. Below the minimum dry film thickness, typically a few mils, the crosslink density never reaches its design level: the finish feels dry but remains soft enough to dent with a fingernail, and household chemicals that should bead up instead stain. Above the maximum, the surface cures and skins while solvent remains trapped beneath; the trapped solvent eventually forces its way out, causing bubbling, or the thick film's internal cure stresses exceed its adhesion, causing cracking and delamination.
Measuring Wet Film Thickness
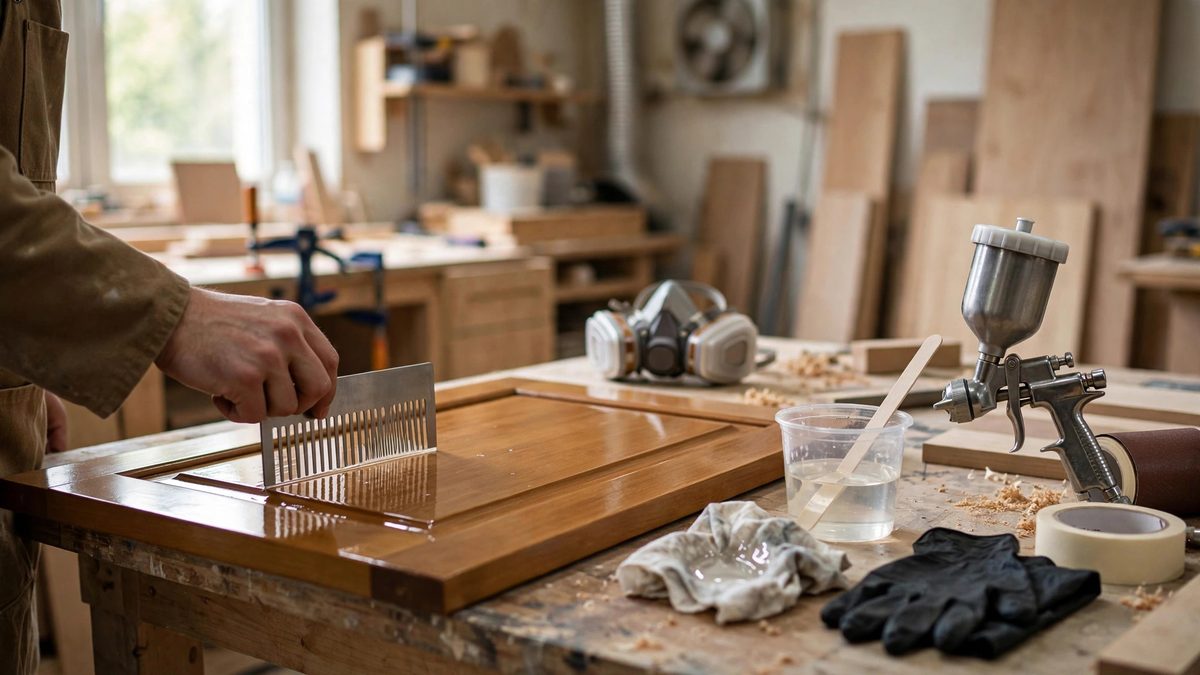
The practical measurement is wet film thickness, taken immediately after spraying with a wet film gauge: a notched comb pressed into the fresh finish, where the highest notch that leaves a mark indicates the thickness. Use it constantly, not occasionally. Establish the target wet thickness from the product's solids content: dry film equals wet film times the volume solids percentage, so a product with 40% volume solids sprayed at 5 mils wet yields 2 mils dry. Check every few pieces and after any gun adjustment, because film thickness drifts with fluid flow, air pressure, gun speed, and overlap without any visible change in how the spray looks. The gauge costs little and takes seconds; skipping it is how a whole run of cabinetry ends up out of spec.
Gun Setup for Consistent Films
Consistent thickness starts with consistent atomization and flow. Set fluid delivery to put down the target wet thickness in a single pass at your natural gun speed and overlap, typically 50% overlap between passes. Too much fluid for your speed means runs and excessive thickness; too little means dry spray and thin films. Atomization pressure affects transfer efficiency and film build: higher pressure atomizes finer but increases bounce-back and overspray, effectively thinning the deposited film while wasting material. Find the lowest pressure that gives acceptable atomization; that maximizes transfer efficiency and makes the deposited thickness predictable. Keep gun distance consistent, because film thickness falls off rapidly with distance. A gun held two inches farther than intended can halve the deposited film without looking dramatically different.
Technique: Speed, Overlap, and Triggering
The sprayer's body is part of the thickness control system. Maintain steady gun speed: speeding up thins the film, slowing down thickens it, and the unconscious tendency is to slow down on edges and details, overbuilding exactly where the finish is already prone to runs. Keep the gun perpendicular to the surface and at constant distance; arcing the wrist at the ends of passes thins the middle and thickens the ends. Overlap each pass by half the fan width for uniform coverage; inconsistent overlap creates stripes of alternating thickness that show as sheen variation in the cured finish. Trigger the gun off the piece at the start and end of each pass: starting the spray on the wood piles material at the entry point, and the correct technique wastes a little finish to the air in exchange for uniform films.
Catalyzation and Pot Life Effects
Conversion varnish is a two-component system, and the catalyst ratio affects viscosity, which affects film build. Mix precisely by the manufacturer's ratio: too little catalyst and the finish under-cures regardless of thickness; too much and the pot life collapses. As the catalyzed material sits, its viscosity rises, and rising viscosity changes the spray characteristics: the same gun settings deposit a thicker, more textured film as the material ages. Respect the pot life strictly and mix only what the session needs; spraying material near the end of its pot life produces films that look okay wet but cure with orange peel, poor flow, and compromised properties. Temperature matters too: cold material sprays thicker, hot material thinner, so condition the finish to shop temperature before spraying.
Safety With Catalyzed Finishes
Conversion varnish contains isocyanates or formaldehyde-releasing catalysts depending on formulation, plus flammable solvents: this is professional material demanding professional precautions. Spray only with proper respiratory protection, supplied-air for isocyanate systems, in a ventilated spray area with explosion-proof electricals. The health effects of sensitization are cumulative and irreversible, which is why the precautions are non-negotiable rather than recommended. Keep a fire extinguisher rated for chemical fires accessible, ground the spray equipment, and store catalyzed leftovers safely, never in sealed containers that pressure can build in.
Film thickness is the variable that makes conversion varnish perform or fail. Measure wet film with a gauge, set the gun for the target build, spray with disciplined technique, respect pot life, and protect your lungs. The finish will cure into exactly what the datasheet promised.
Related Guides
- Hardwax Oil Penetration on Dense Hardwoods: Hardwax oils promise the best of both worlds: the natural look and repairability of an oil with the protection of a wax film. On dense hardwoods like
- Buffing Polyurethane Coats With Pumice and Rottenstone: Brushed polyurethane almost never dries into the flawless surface you want. There are always brush marks, dust nibs, and orange peel to deal with
- Wet Sanding Pre-Catalyzed Lacquer to Mirror Luster: Pre-catalyzed lacquer is the finish of choice when you want durability with a fast build, but straight off the gun it usually carries a fine
- Spray Viscosity Tuning for Two-Part Polyurethane Coats: Two-part polyurethane lays down a hard, chemical-resistant film that furniture makers love, but it only sprays well within a narrow viscosity window