
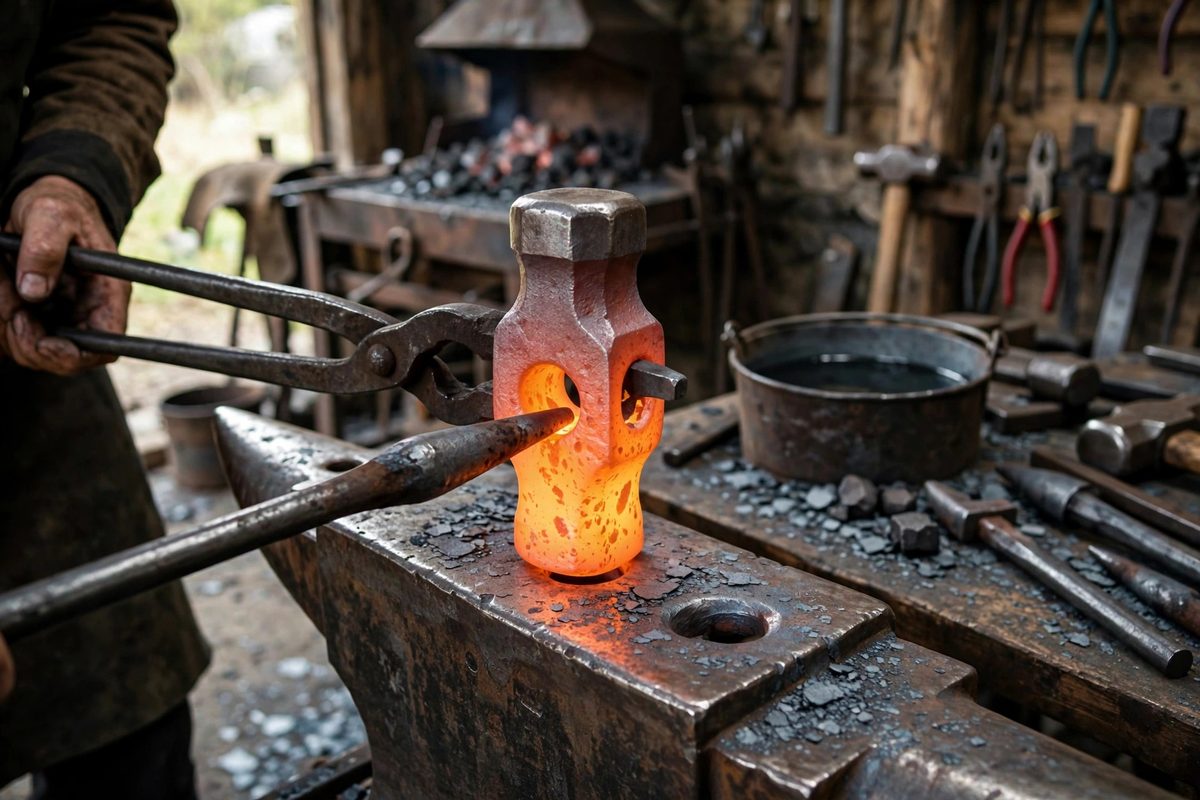
Forging a hammer head means making an eye: the hole through which the handle passes, and the most structurally critical feature of the tool. The traditional method punches the hole hot with a punch and then drifts it, enlarging and shaping it with a tapered drift, to final size. Punching and drifting displace metal rather than removing it, which keeps the grain flowing around the eye instead of cutting across it, and that grain flow is what makes a forged eye stronger than a drilled one. It is demanding work at high heat, but it is the heart of hammer making.
Why punch instead of drill
Drilling an eye removes metal and severs the grain structure, leaving cut grain ends around the hole that act as stress risers. Punching pushes the metal aside: the material that would have been the hole gets displaced into the surrounding head, actually adding mass around the eye where strength is needed most. The grain flows around the punched hole in continuous lines, the way grain flows around a knot in wood, which resists the splitting forces the handle exerts. For a tool that will endure thousands of impacts, this matters. Drifting then shapes the displaced opening into the precise tapered form the handle needs. The punched-and-drifted eye is not just traditional; it is mechanically superior, which is why the method survives in an age of machine tools.
Punching at the right heat
Punch at a full welding heat: the steel should be bright yellow, nearly white, the hottest you can manage without burning it. Tool steel needs this heat because punching at lower temperatures risks cracking, especially in higher-carbon steels. Support the head on the anvil or a bolster plate with a hole or slot beneath the punching point, so the punched slug has somewhere to go. Drive the punch with firm, committed hammer blows, or with a striker if you have one, keeping the punch vertical; a leaning punch makes a leaning hole that the drift cannot fully correct. Punch about halfway through from one side, then flip the head and punch from the other side to meet in the middle. This two-sided approach keeps the hole centered and prevents the exit side from blowing out raggedly. Knock the slug out and inspect: the hole should be roughly centered and reasonably straight.
Drifting to size and shape
The drift is a tapered steel bar, shaped to the eye's final cross-section: usually a rounded rectangle, wider in the middle, sized so the handle will wedge tightly. Drive the drift through the punched hole at forging heat, working it back and forth and rotating slightly, enlarging the hole to the drift's dimensions. The drift does double duty: it sizes the hole and it smooths and compacts the interior surface, work-hardening the eye walls favorably. Keep the head at heat throughout drifting; drifting cold steel cracks eyes. Check the drift's progress frequently, measuring against the handle or a template, because overshooting means a loose eye, and there is no un-drifting. The eye should end up slightly tapered, wider at the top where the wedge will expand the handle, which is the geometry that locks the handle permanently.
Handle fit and wedging
The drifted eye and the handle are a matched pair. Fit the handle by shaping it to enter the eye snugly from the bottom, seating firmly with hand pressure and a few taps; it should not rattle or rock. The handle's top should protrude slightly above the head. Drive a wooden wedge into the saw kerf in the handle's top, expanding the handle against the eye's taper, and follow with a metal wedge crosswise for insurance. The wedge system works because the eye tapers: the expanded handle cannot pull back through the narrower bottom. Test the hang by feel; a well-hung hammer feels like one piece, with no shift or rattle on impact. Oil the handle and let the assembly settle before heavy use.
Safety at the anvil
Punching and drifting concentrate every forge hazard: maximum heat, heavy hammer blows, flying scale, and a punch or drift that can glance off. Eye protection is mandatory, and a face shield is wise when striking punches. If working with a striker, establish clear communication: the striker strikes only on the smith's command and stops instantly on the command to stop. Keep the punch and drift handles in good condition; a loose handle on a hot punch is a projectile. Quench the punch and drift periodically during use to protect their temper, and keep a clear floor around the anvil so a dropped hot tool lands on dirt, not on a foot. The work is intense but brief; give it your full attention for the minutes it takes.
Punch hot from both sides, drift to a tapered fit at heat, hang the handle with wedges, and respect the violence of the process. The punched eye is the signature of a real forged hammer, stronger for being displaced rather than drilled.
Related Guides
- Hardening Drift Punches With Differential Water Dips: A drift punch needs a hard working tip and a tough body that can take hammer blows without shattering. Hardening the whole punch uniformly makes it
- Heat Treating Shock Resistant S7 Steel Cold Chisels: S7 is the shock-resistant tool steel, formulated to absorb impact without chipping or shattering, which makes it the natural choice for cold chisels
- Hardening Face Plates on Heavy Anvil Horns: A blacksmith's anvil takes thousands of hammer blows, and its working faces must be hard enough to resist denting while the body stays tough enough
- Sharpening Hand Forged Drawknives on Stones: The drawknife, pulled toward the user to shave wood, is one of the oldest edge tools, and a hand-forged one carries the smith's geometry in its