
Snap-fit tabs are the 3D printer's answer to screws: a cantilever beam that bends aside during assembly and springs back to lock parts together. They are elegant, cheap, and easy to get wrong. The difference between a tab that clicks satisfyingly for years and one that snaps on the third assembly is deflection math, and PETG's particular personality as a material shapes every number. Designing snap fits for printed PETG means respecting both the beam equations and the reality that a printed beam is not the same as a molded one.
How a cantilever snap fit works
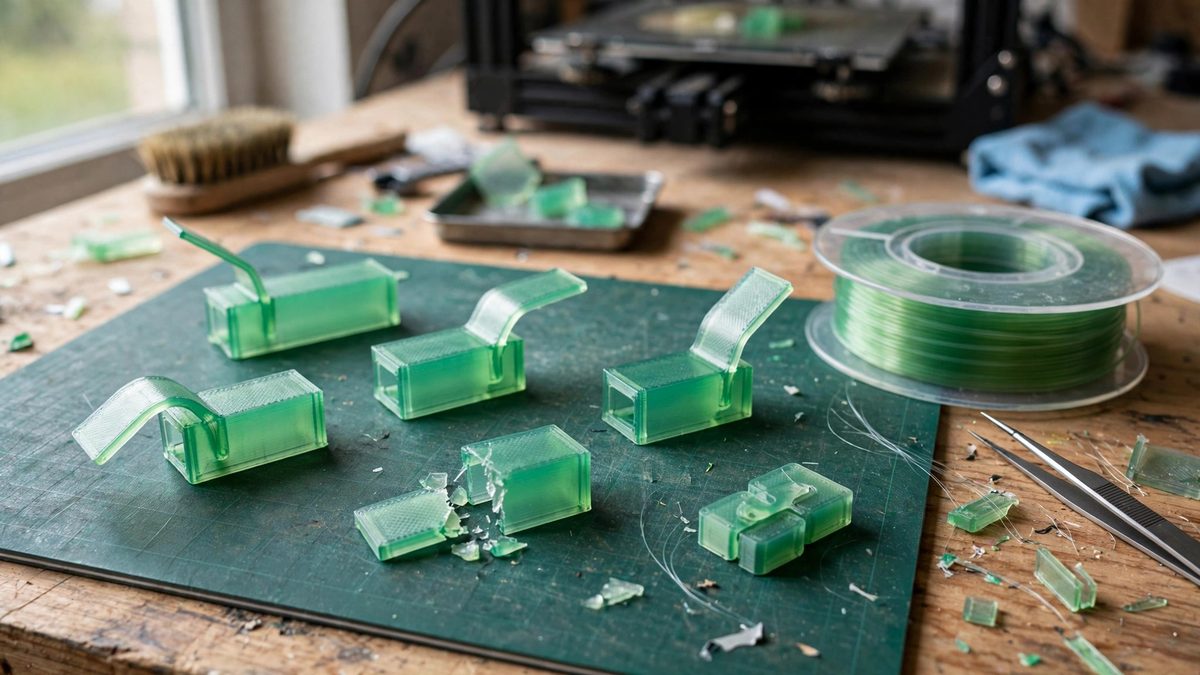
A snap-fit tab is a beam fixed at one end and free at the other, with a hook or ramp near the free end. During assembly, the mating part pushes the beam sideways; the beam bends, the hook passes the catch, and the beam springs back. The critical design variable is how far the beam tip deflects during that pass, relative to what the material can tolerate. The classic beam relationship says deflection grows with the cube of beam length and shrinks with the cube of beam thickness: a beam twice as long deflects eight times as far under the same load, while a beam twice as thick deflects one-eighth as far. This cubic sensitivity is why small dimensional changes in your model produce dramatic changes in how the tab feels. Length is your friend for easy assembly; thickness is your friend for holding strength; the design balances the two.
PETG's strain personality
PETG is tougher and more flexible than PLA, which makes it a natural choice for snap fits that must survive repeated use. Where PLA tabs tend to snap from brittleness, PETG tabs tend to survive by bending further. But PETG has limits too. As rough shop guidance, keep the maximum fiber strain in the beam around one to two percent for tabs that will be assembled many times; occasional-assembly tabs can push somewhat higher. Strain at the beam root relates directly to deflection: for a rectangular beam, the maximum strain is roughly proportional to the thickness times the deflection divided by the length squared. The practical takeaway is that long, thin beams are gentle on the material and short, thick beams are brutal. If a tab feels like it requires heroic force to assemble, the beam is too short or too thick for the required deflection, and the material is telling you so before it fails.
Design rules that keep tabs alive
Several detailing rules separate durable snap fits from doomed ones. Put a generous fillet at the beam root, because the root is where stress concentrates and a sharp inside corner is where cracks start; a fillet radius of roughly half the beam thickness is a good starting point. Taper the beam slightly, thicker at the root and thinner toward the tip, so the bending stress distributes along the length instead of peaking at the base. Keep the hook or ramp modest: the deflection the beam must achieve equals the hook height, so a tall hook demands more bend than a shallow one. Add a lead-in angle on the mating part so assembly force ramps up gradually instead of hitting the tab like a hammer. And design the catch with a small clearance so the beam returns to nearly its undeflected position when locked; a beam held permanently bent will creep over time and lose its grip.
The printed-versus-molded reality
Here is the catch: beam equations assume a solid, isotropic material, and a 3D print is neither. Layer lines run perpendicular to the beam in the worst orientation, and the beam's strength across layers is a fraction of its strength along them. Orient the tab so bending stresses run along the layers, not across them: print the beam lying flat so the layers stack through the thickness, putting the layer boundaries parallel to the bending plane rather than across it. Use enough perimeters that the beam's outer skin, which carries the highest stress, is solid material; four or more perimeters is a sensible starting point for functional tabs. Infill matters less than perimeters for thin beams, since a thin beam is mostly skin anyway. Then prototype and test to destruction, because the only honest deflection tolerance for your printer, your filament, and your geometry is the one you measure.
Testing and iterating
Print the tab as a standalone test coupon before committing it to a full part. Assemble and disassemble it repeatedly, counting cycles, and watch for whitening at the root, which signals the material is yielding even if it has not broken yet. If it breaks, lengthen the beam or thin it slightly; if it assembles too easily and feels loose, shorten or thicken. Change one variable at a time. Keep notes on what worked, because snap-fit feel is hard to remember precisely and your future self will thank you. A small library of proven tab geometries, tested on your own machine, becomes one of the most reused assets in your STL collection.
Snap fits reward the designer who thinks in beams rather than shapes. Get the deflection right for PETG's strain limits, orient the print to favor the layers, and the tab will click into place like it was always meant to be there.
Related Guides
- Printable Snap Joint Clearances for Hard Polycarbonate: Snap-fit joints, the cantilever hooks and annular rings that click assemblies together without fasteners, are among the most satisfying features to
- Chamfer Relief Clearance for Friction Fit Printable Pins: Printed pins that press into printed holes are the bread and butter of 3D-printed assemblies: hinges, joints, locators, fasteners. Getting the
- Calculating Living Hinge Deflection in TPU Parts: A living hinge, a thin flexible section printed as part of the whole, lets a 3D-printed part bend repeatedly without hardware. In TPU, the flexible
- Living Hinge Fatigue Calculations for TPU Prints: A living hinge printed in TPU is one of those designs that either lasts years or snaps in a week, and the difference is geometry, not luck. Unlike